Industrial-Grade Camera Module Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000

industrial-grade camera module

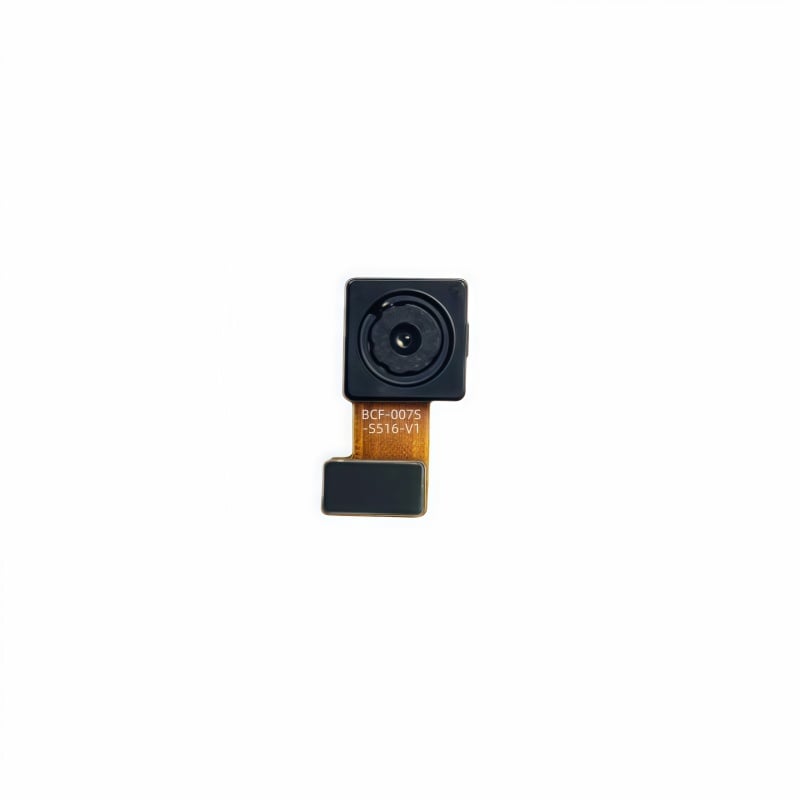
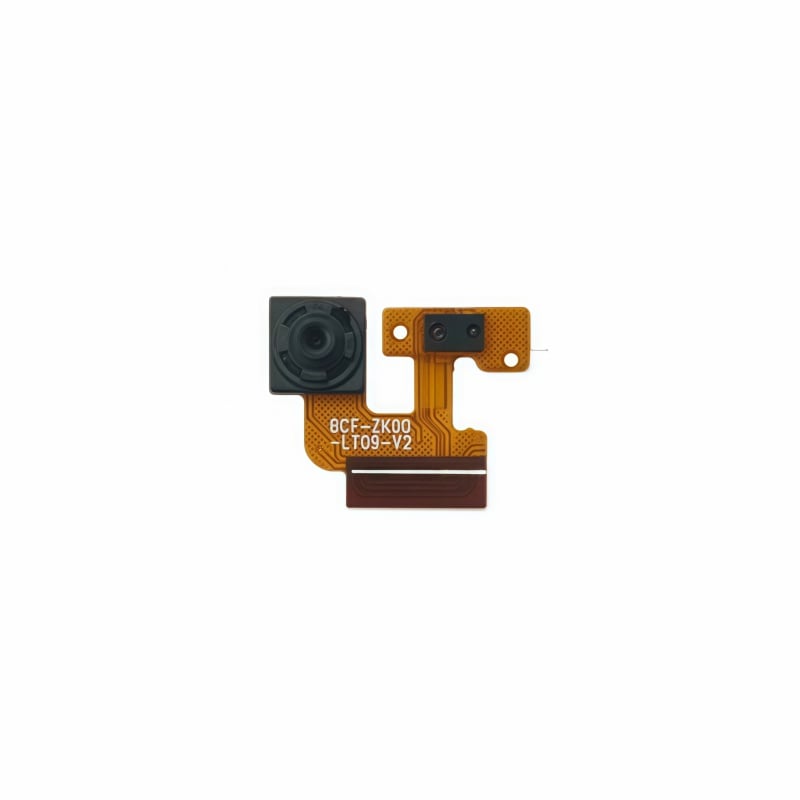
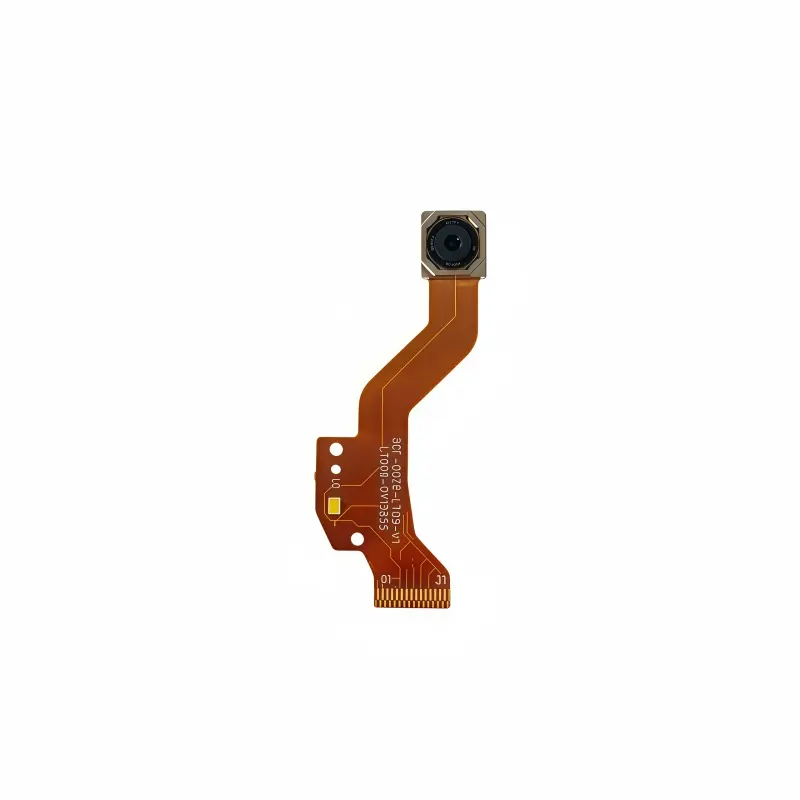
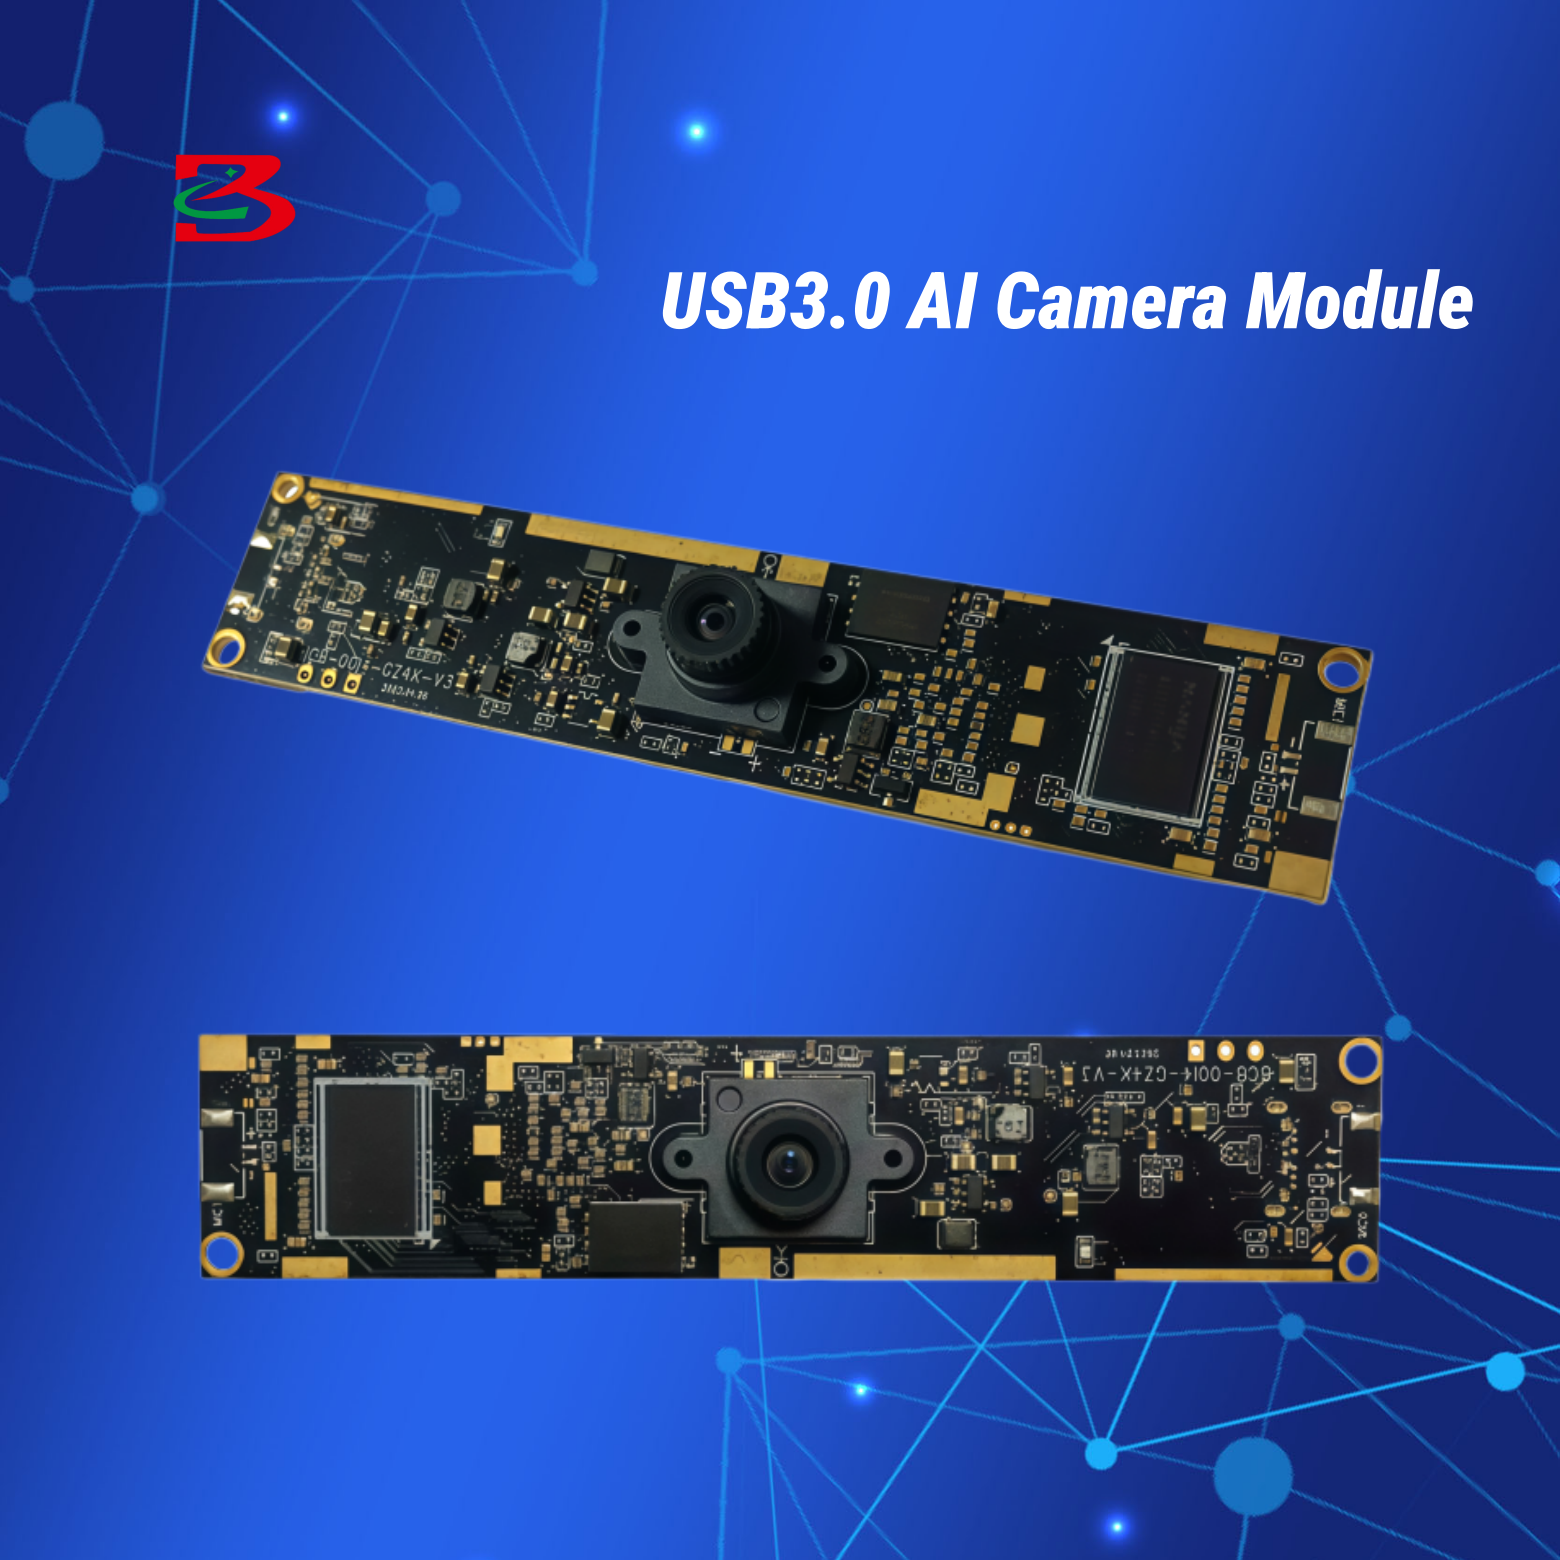
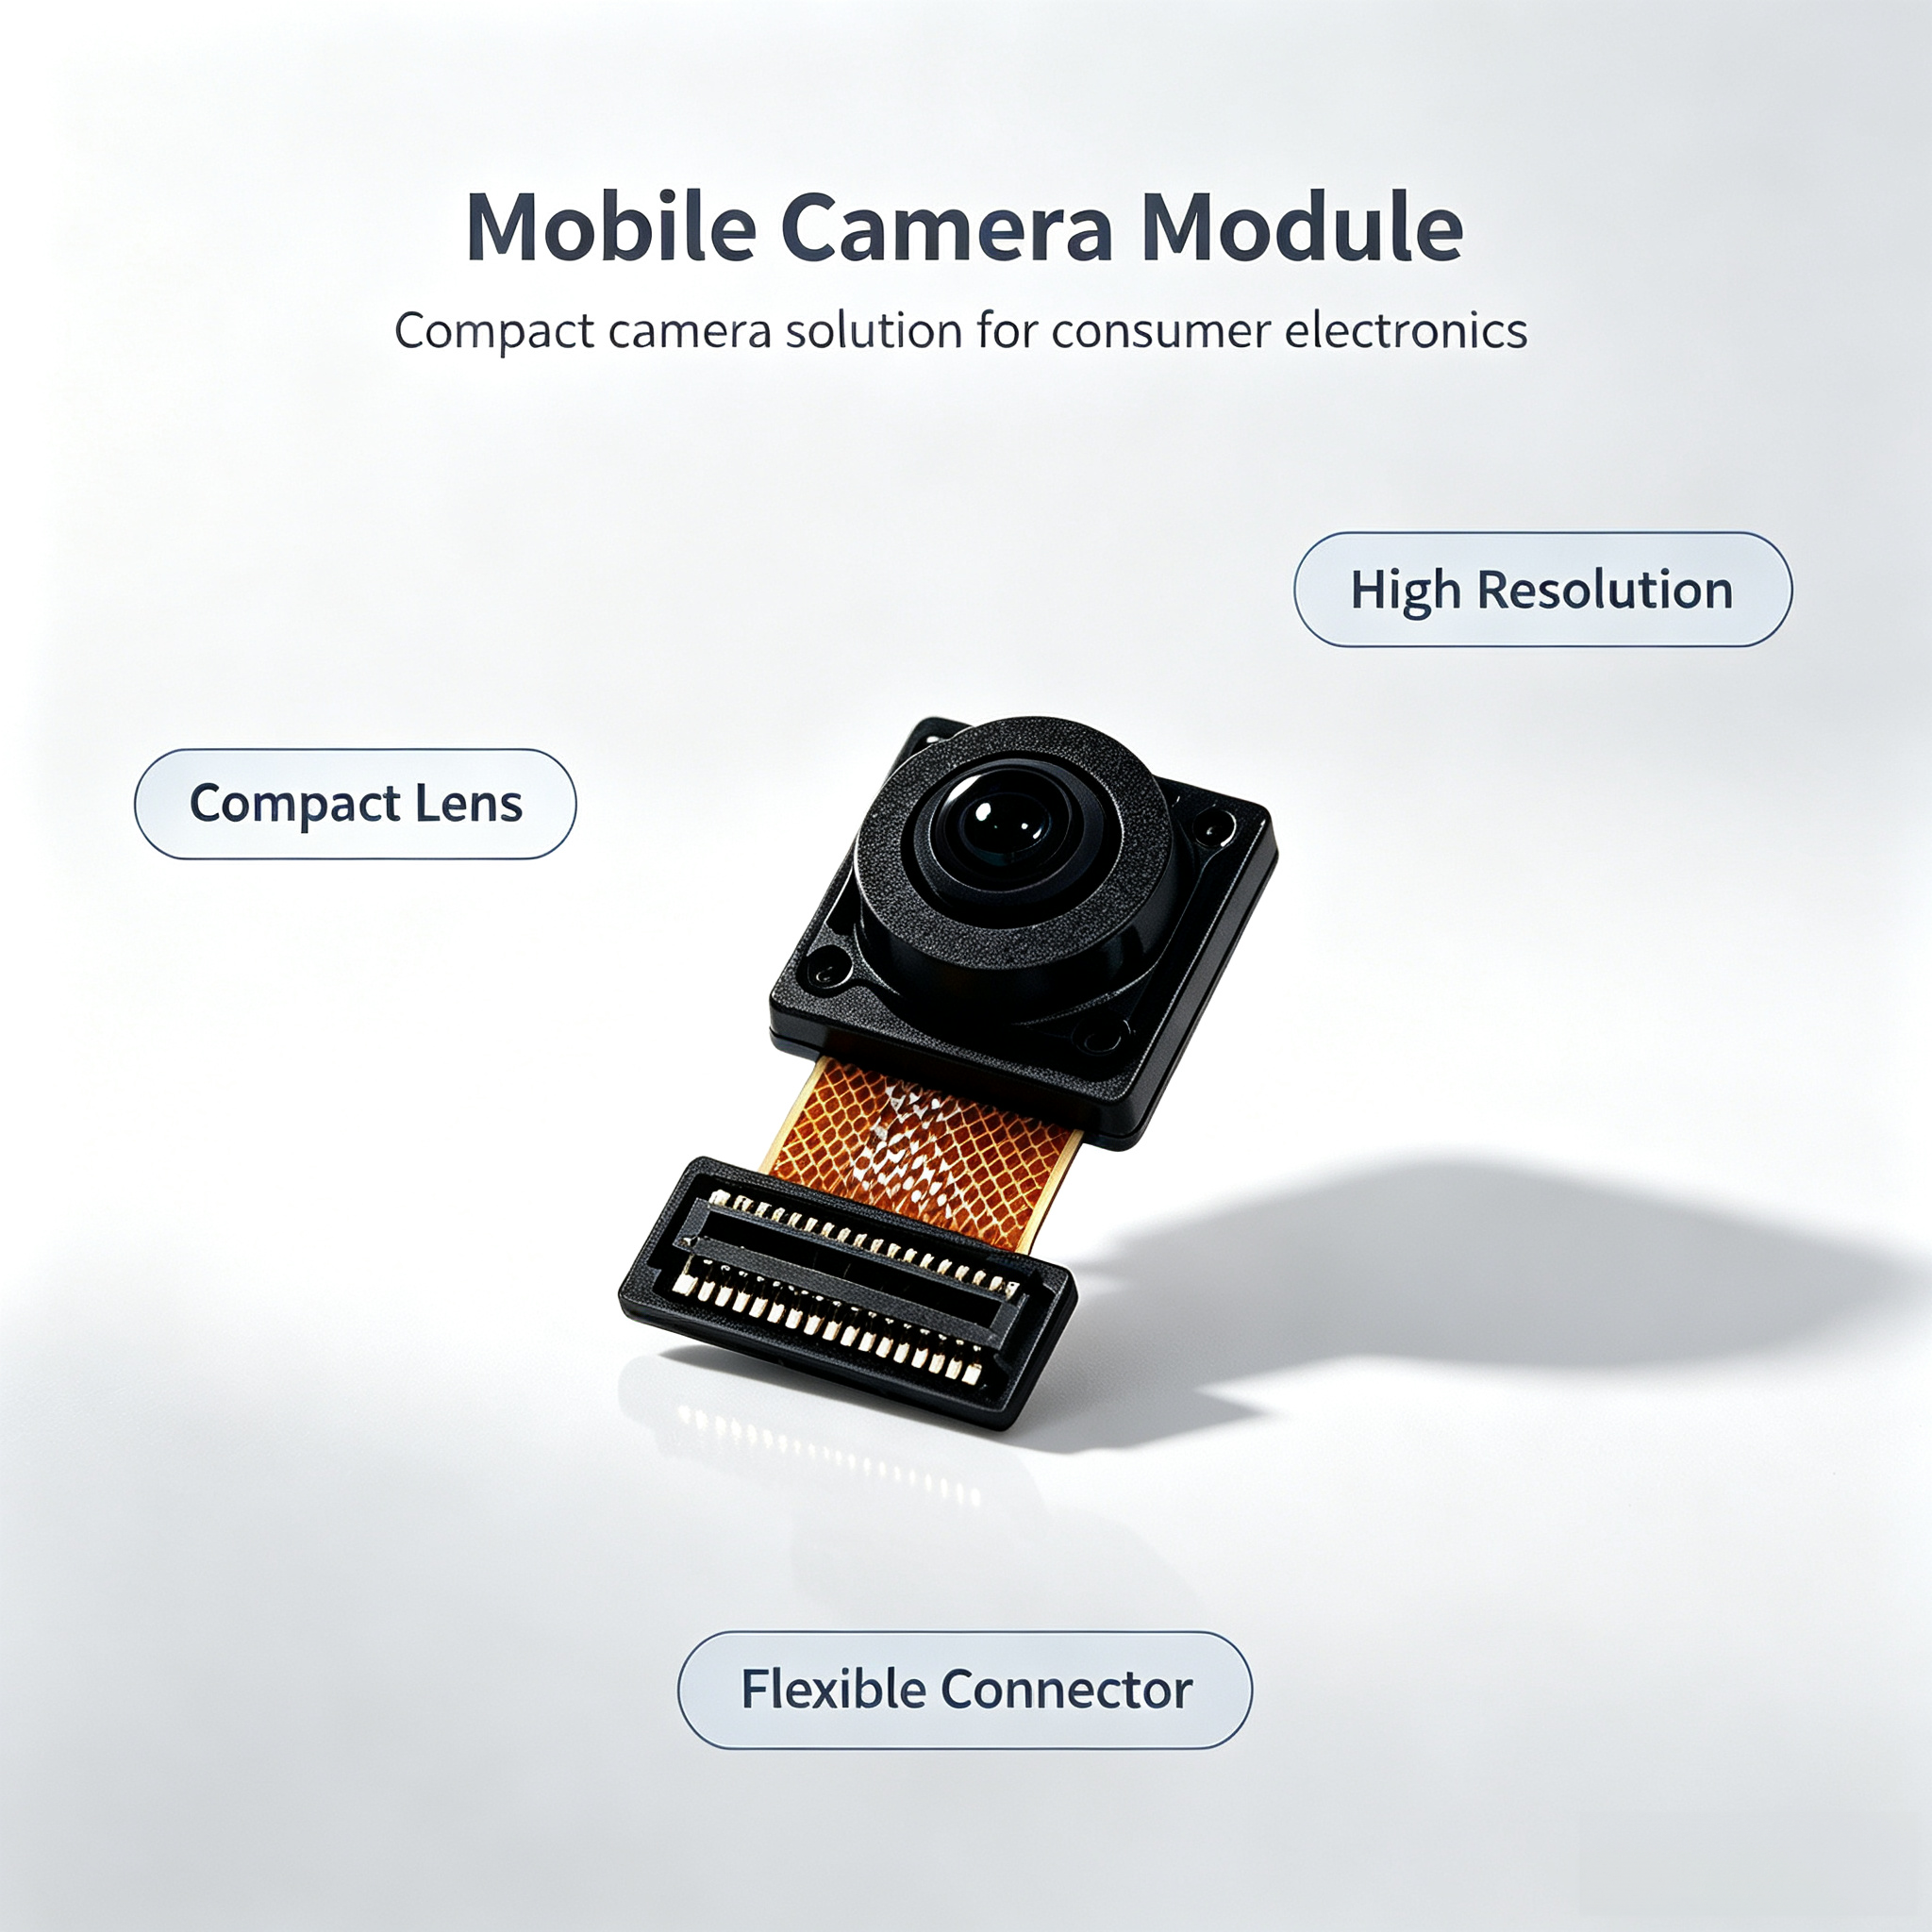
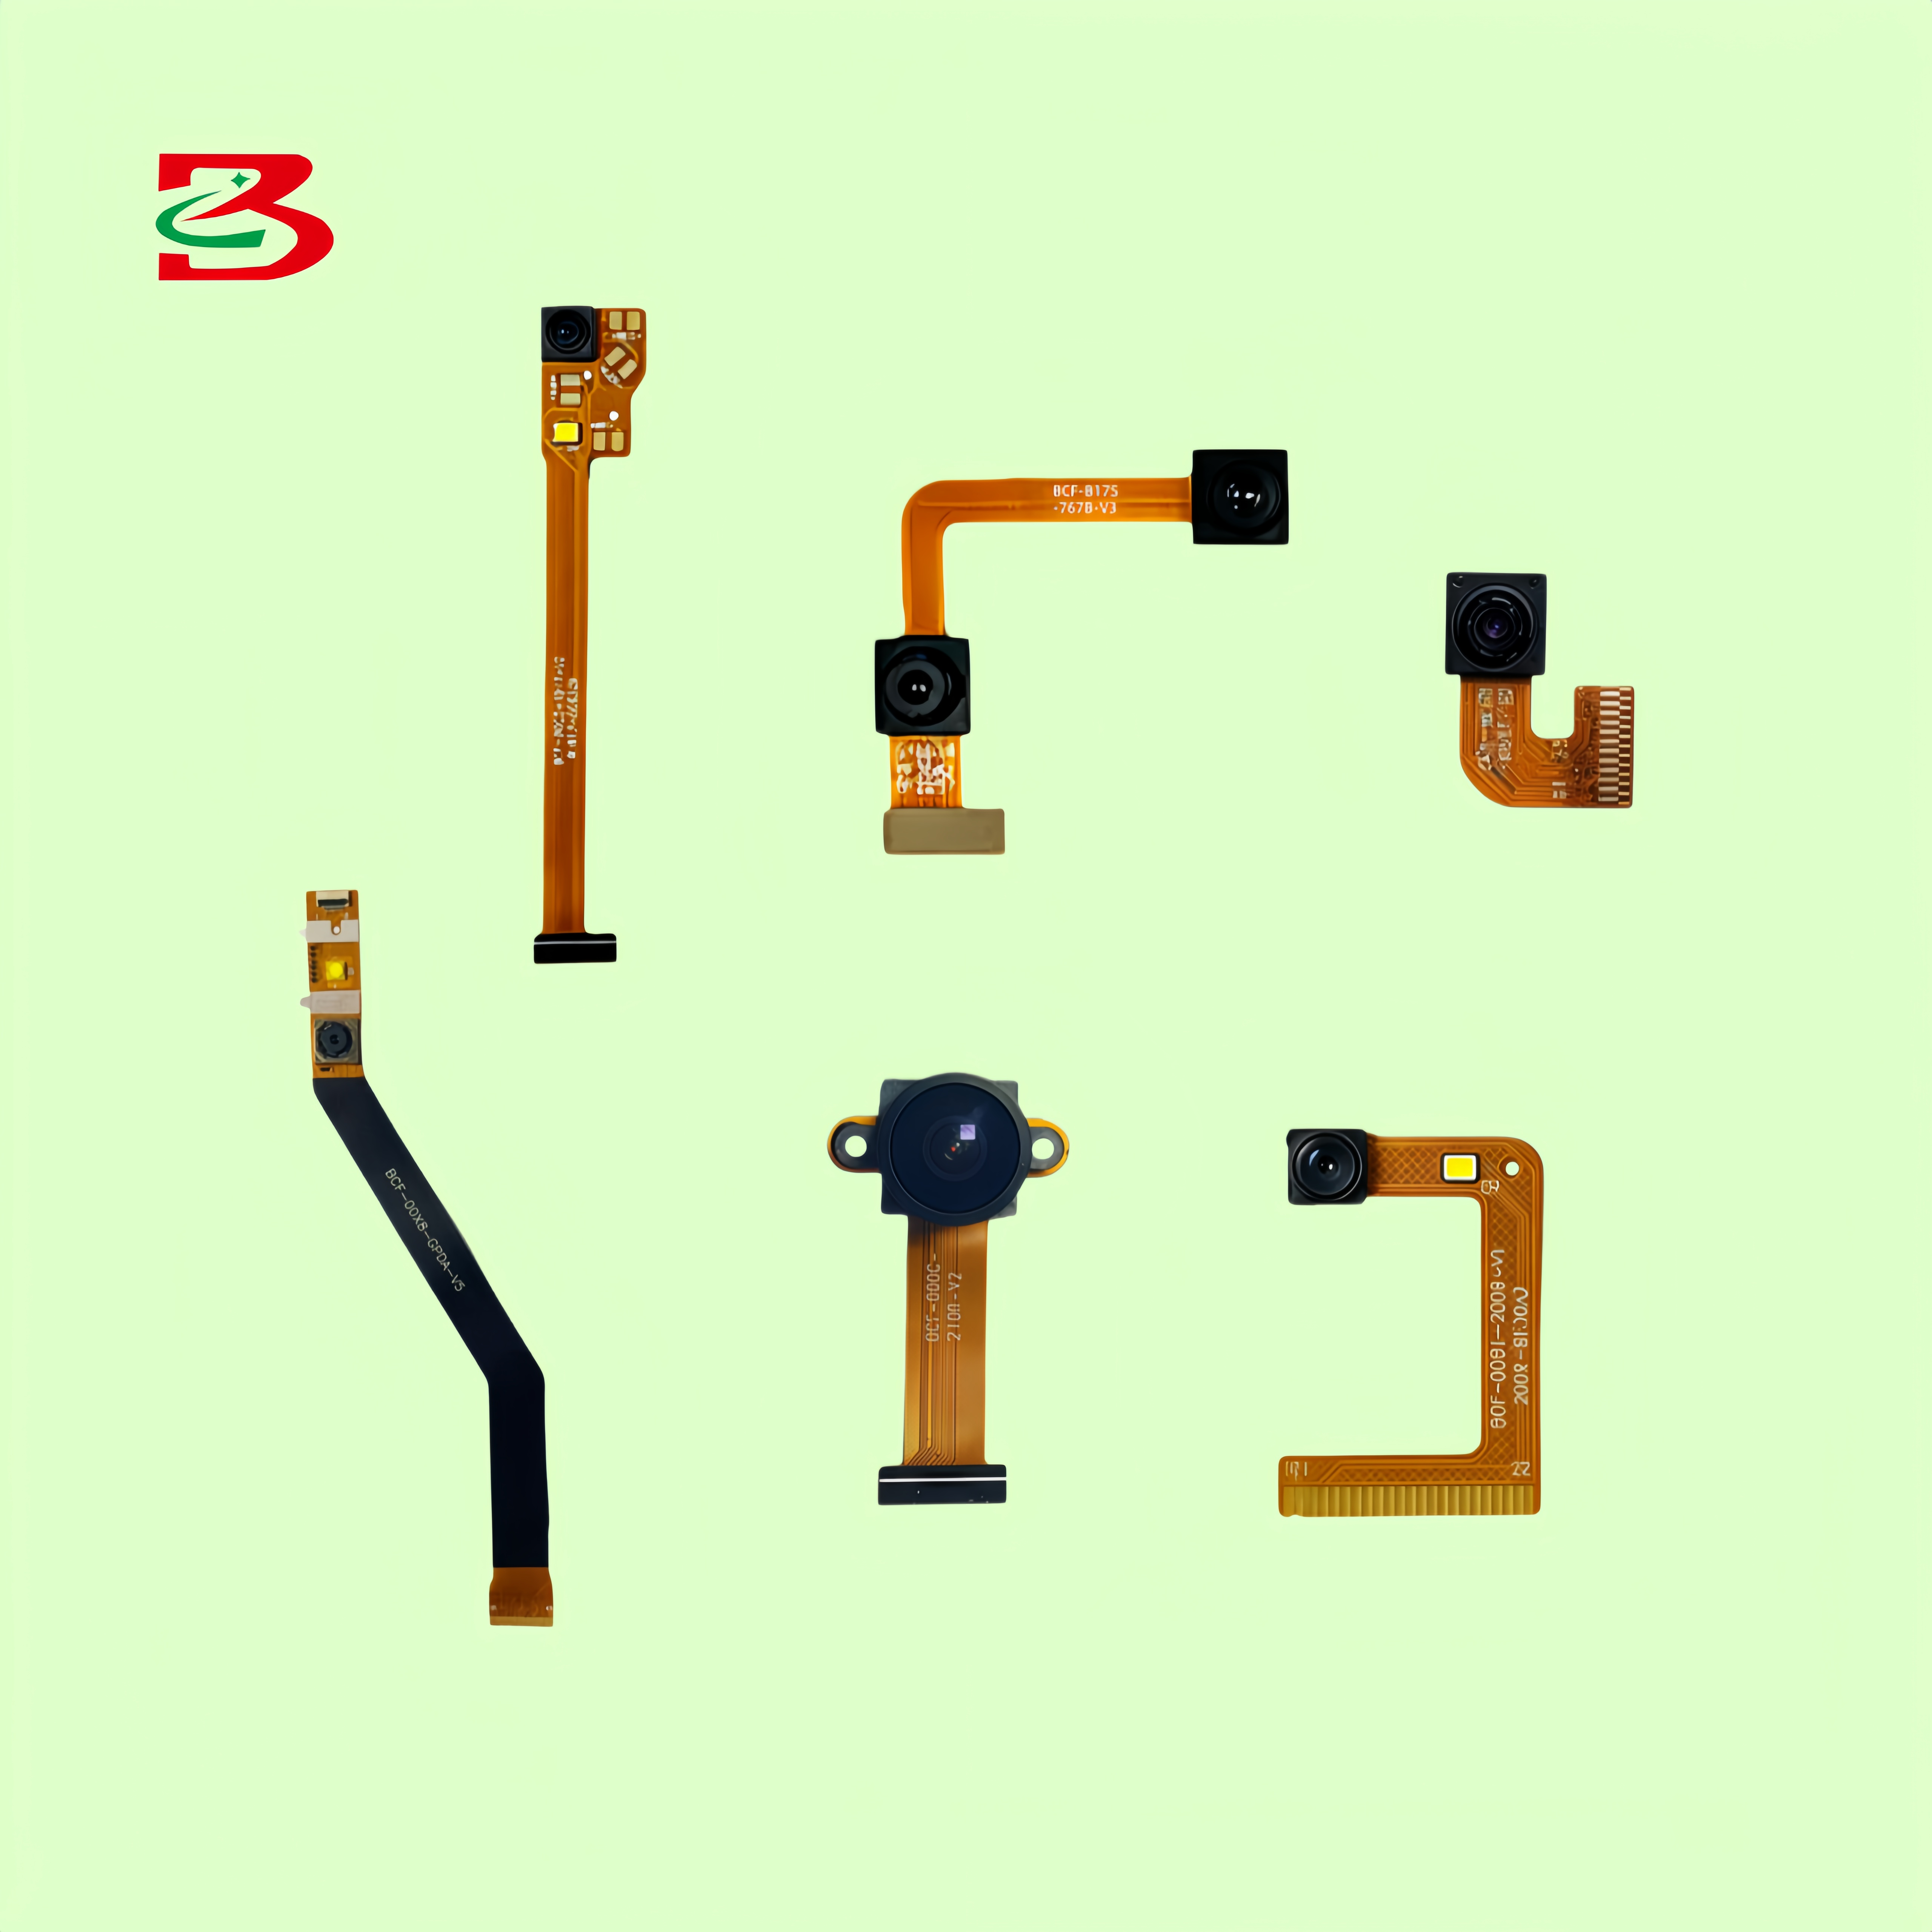
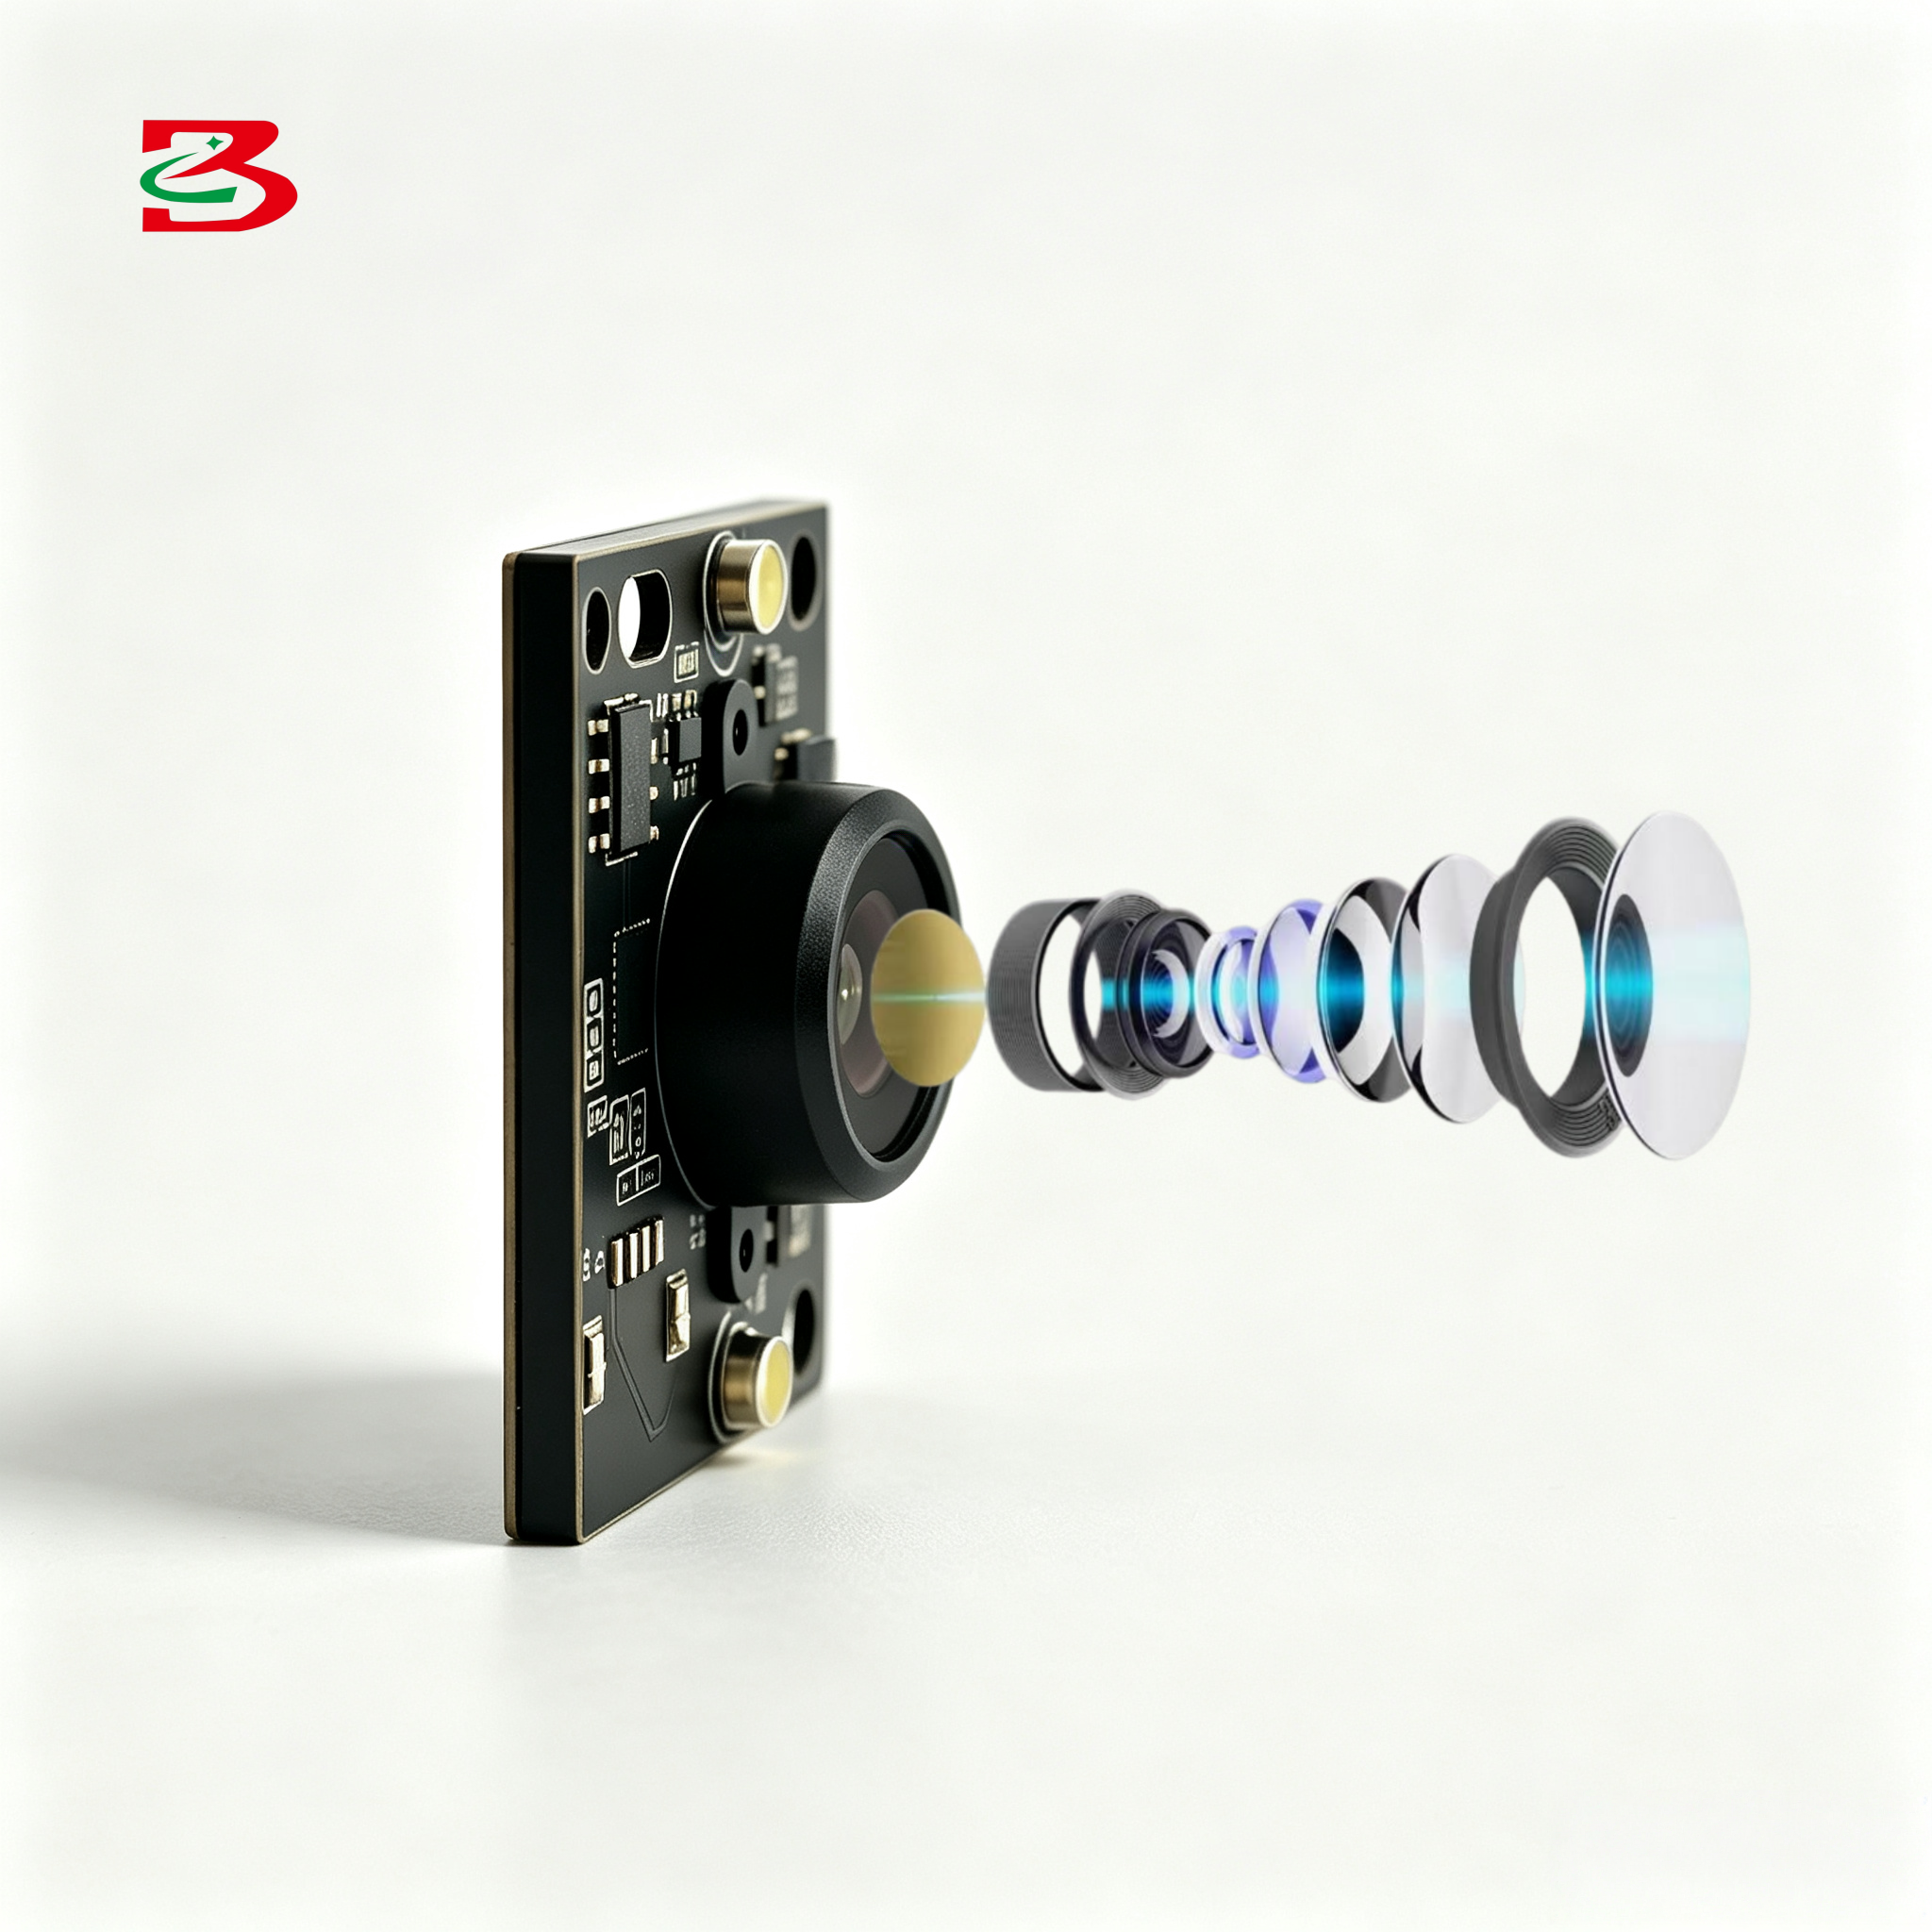
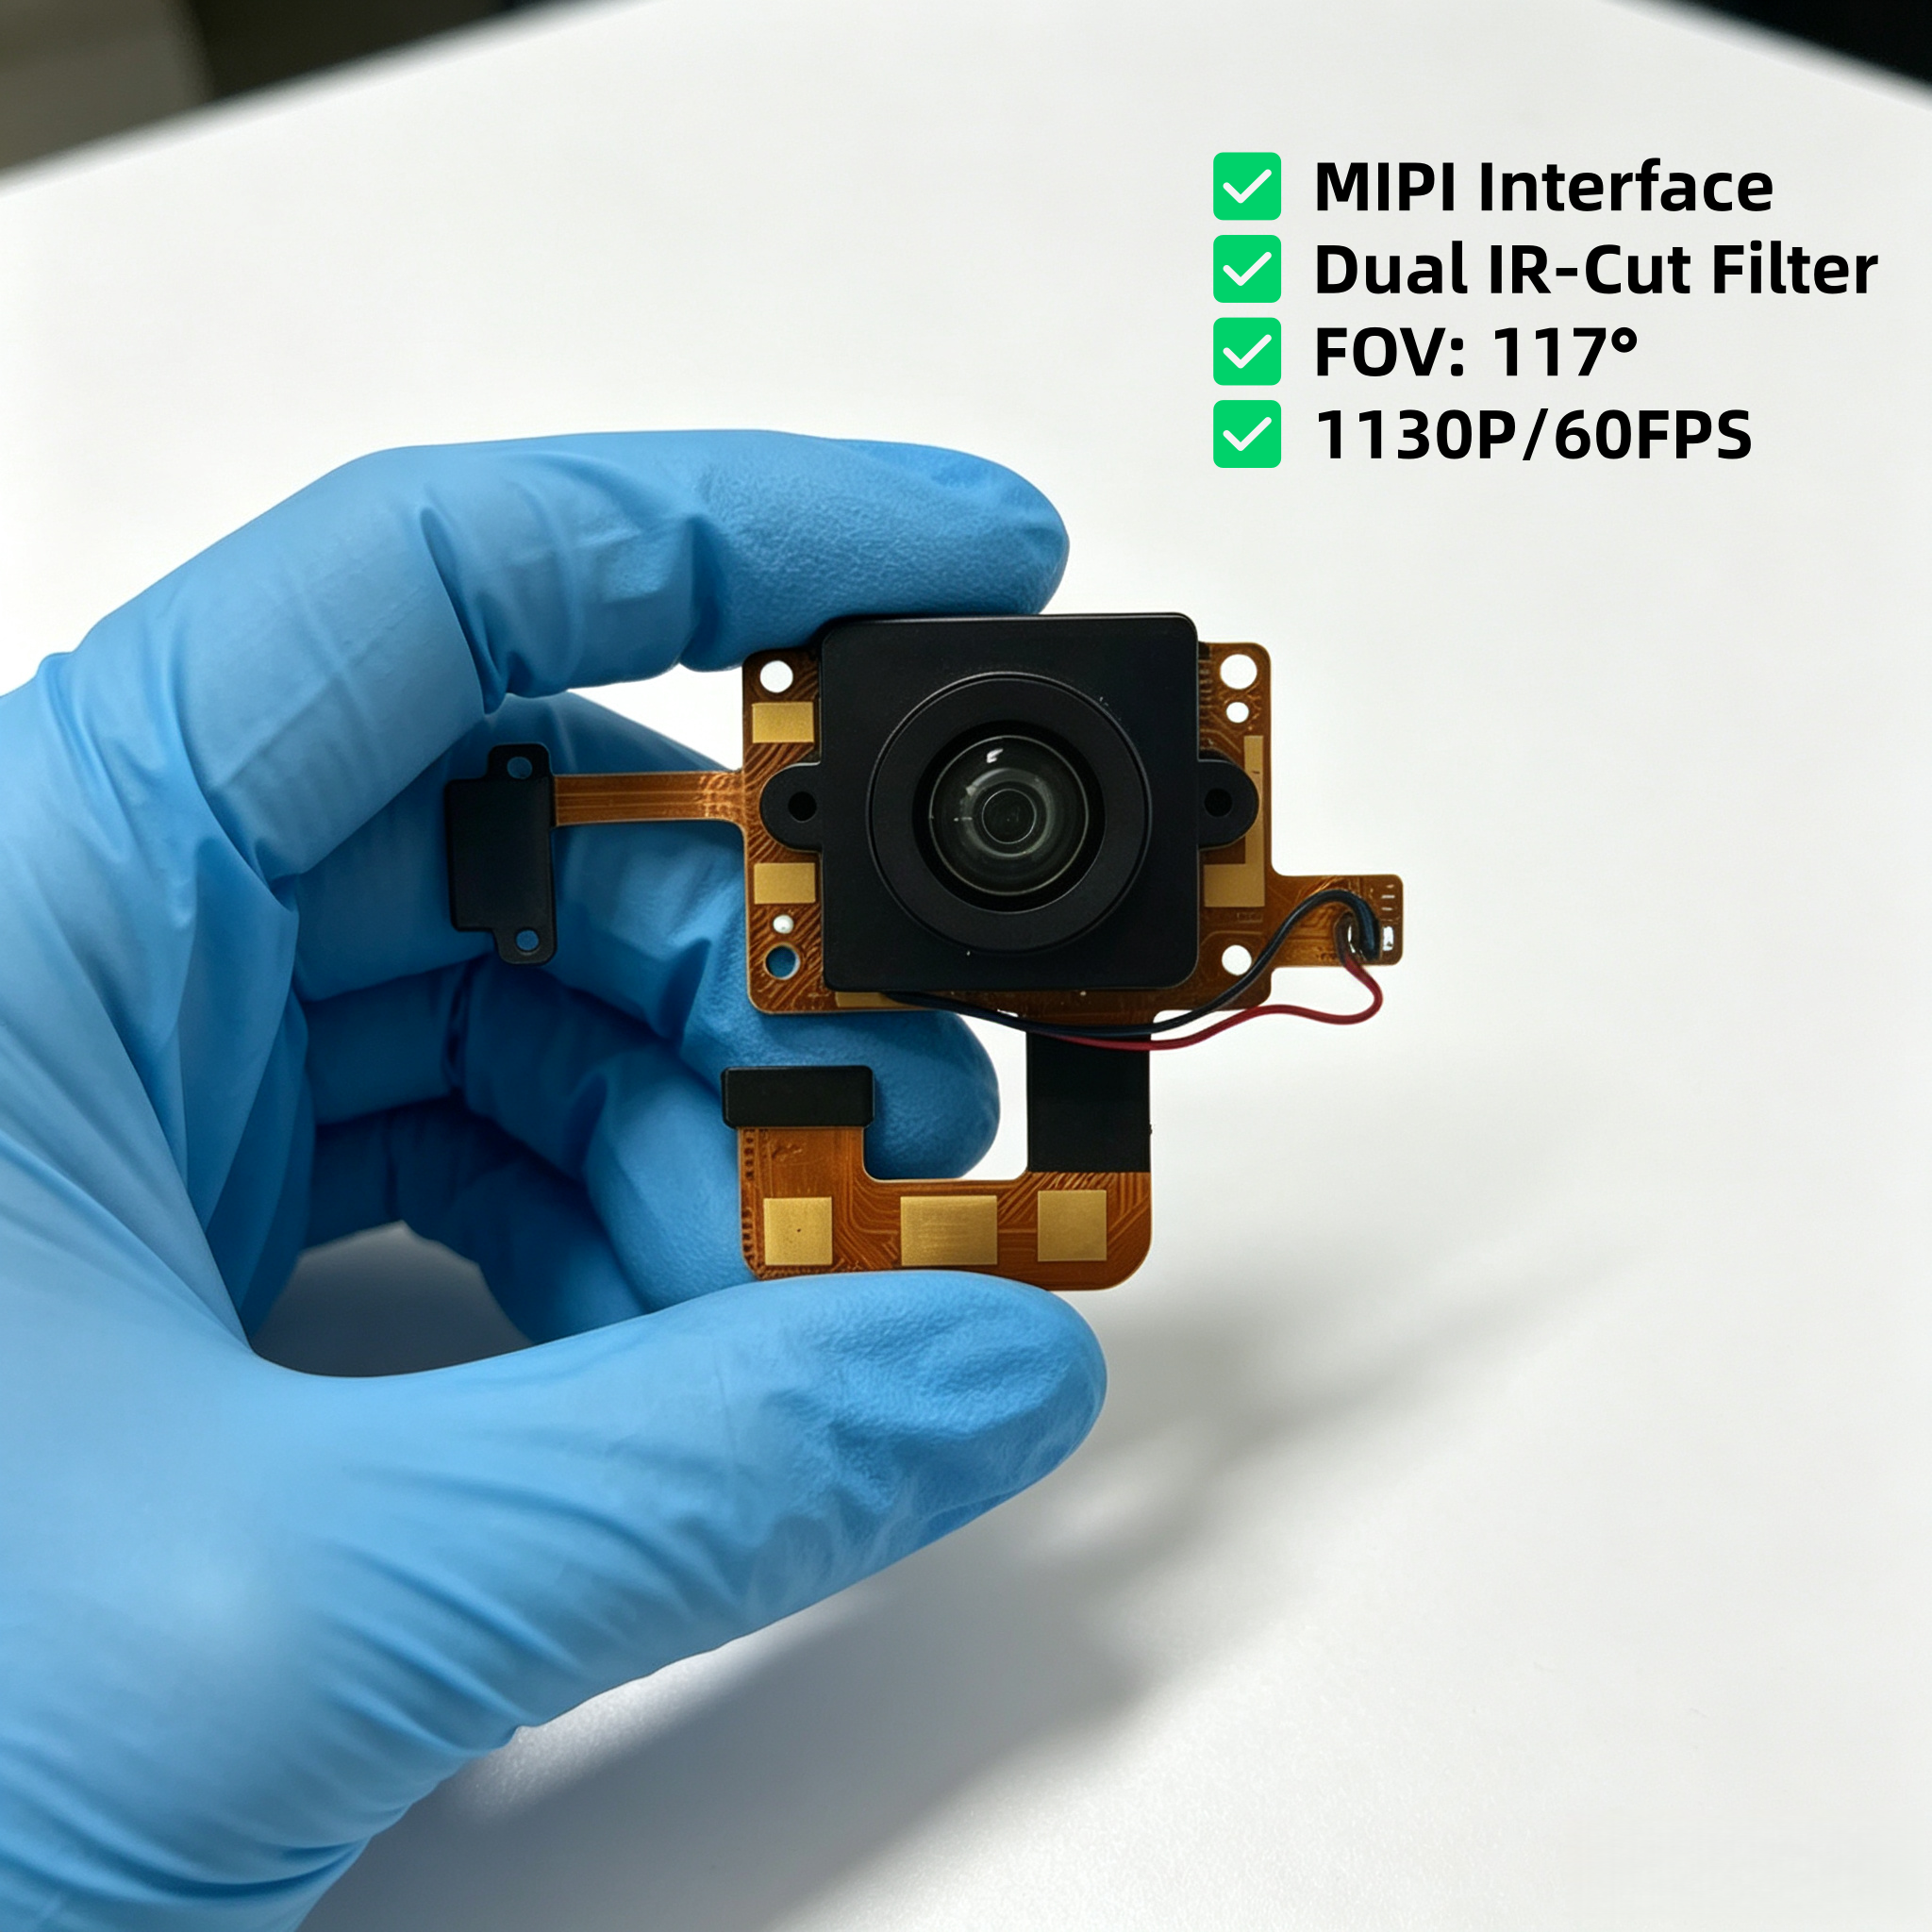
An industrial-grade camera module represents a sophisticated imaging solution designed for demanding professional environments where reliability and precision are paramount. This specialized industrial-grade camera module integrates advanced optical components with robust electronic systems to deliver exceptional performance in challenging conditions. The primary functions of an industrial-grade camera module include high-resolution image capture, real-time video processing, and seamless integration with automated inspection systems. Technologically, these modules feature cutting-edge sensors that operate across extended temperature ranges, sophisticated noise reduction algorithms, and standardized interfaces for easy system integration. An industrial-grade camera module typically incorporates global shutter technology, ensuring distortion-free image capture even during rapid motion or vibration. The optical design provides excellent light gathering capability with minimal aberration, while the mechanical construction withstands harsh industrial environments including dust, moisture, and temperature fluctuations. Applications for an industrial-grade camera module span manufacturing quality control, machine vision inspection, robotics guidance systems, surveillance networks, and scientific research. The versatile nature of an industrial-grade camera module makes it indispensable across pharmaceutical production, automotive assembly, electronics manufacturing, and food processing industries where visual inspection standards are non-negotiable.

Popular Products

The industrial-grade camera module delivers substantial operational benefits that directly enhance productivity and reduce operational costs across manufacturing facilities. Users experience significant advantages through the module's ability to function reliably in extreme temperature environments, eliminating downtime caused by equipment failure. The industrial-grade camera module provides exceptional image clarity that enables precise defect detection, preventing substandard products from reaching customers and protecting brand reputation. This advanced technology allows facilities to automate inspection processes, reducing labor costs while improving consistency and accuracy beyond human capability. The industrial-grade camera module's standardized connectivity options simplify integration into existing production infrastructure, minimizing installation expenses and technical complications. Purchasing an industrial-grade camera module represents a smart investment because the extended operational lifespan offsets initial expenditure through years of dependable service. The module's superior light sensitivity enables effective inspection under variable lighting conditions without additional expensive supplementary lighting systems. Industrial facilities benefit from the industrial-grade camera module's built-in redundancy features and fail-safe mechanisms that prevent production line interruptions during critical operations. The straightforward calibration process of an industrial-grade camera module allows technical teams to deploy systems quickly without extensive training or specialized expertise. Real-world applications demonstrate that companies implementing this industrial-grade camera module achieve measurable improvements in quality metrics while simultaneously reducing scrap rates and rework expenses. The investment in an industrial-grade camera module ultimately translates into enhanced competitiveness and stronger profitability through improved operational efficiency.

Tips And Tricks

Face Recognition Cameras vs Ordinary Cameras: What Are the Core Differences?

01

Jul

Face Recognition Cameras vs Ordinary Cameras: What Are the Core Differences?

Face recognition cameras and ordinary cameras serve fundamentally different purposes in modern security and surveillance systems. While ordinary cameras simply capture video footage for later review, face recognition cameras actively identify and ana...
View More
Megapixels Do Not Equal Image Quality: A Guide to Avoid Pitfalls When Choosing Camera Modules

13

Jul

Megapixels Do Not Equal Image Quality: A Guide to Avoid Pitfalls When Choosing Camera Modules

When evaluating imaging solutions for industrial applications, security systems, or embedded devices, many decision-makers assume that higher megapixel counts automatically translate to superior image quality. This assumption has become one of the mo...
View More
Full Parameter Guide of Low-Light Camera Modules for Face Recognition Access Control

10

Aug

Full Parameter Guide of Low-Light Camera Modules for Face Recognition Access Control

Low-Light Camera Modules are essential components in modern face recognition access control systems, enabling reliable identity verification even in challenging lighting conditions. As security infrastructure becomes increasingly sophisticated, under...
View More
One-Stop OEM Service for Optical Lenses: Customizable Focal Lengths & Interfaces

20

Aug

One-Stop OEM Service for Optical Lenses: Customizable Focal Lengths & Interfaces

Optical Lenses serve as the foundation for countless imaging, sensing, and optical systems across industries. Whether you are developing a medical imaging device, industrial inspection system, or consumer camera module, the quality and customization ...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000

industrial-grade camera module

Exceptional Durability in Harsh Environments

Exceptional Durability in Harsh Environments

An industrial-grade camera module stands apart through its exceptional durability and rugged construction specifically engineered for harsh industrial environments. The module withstands extreme temperature variations ranging from sub-zero conditions to high-heat environments without performance degradation or image quality loss. Unlike consumer-grade alternatives, an industrial-grade camera module incorporates sealed optical pathways and protective coatings that resist corrosion from chemical exposure, dust infiltration, and moisture accumulation. The industrial-grade camera module's mechanical housing utilizes premium materials selected for longevity and dimensional stability under constant vibration stress. This robust construction ensures consistent imaging performance throughout multi-year operational cycles without requiring frequent recalibration or replacement. Facilities investing in an industrial-grade camera module experience dramatically reduced maintenance overhead and unplanned downtime. The sealed design of an industrial-grade camera module enables deployment in food processing areas, pharmaceutical cleanrooms, and chemical manufacturing zones where contamination resistance proves absolutely critical for regulatory compliance and product integrity.
Superior Image Quality and Advanced Processing

Superior Image Quality and Advanced Processing

The industrial-grade camera module delivers superior image quality through state-of-the-art sensor technology and intelligent processing algorithms that capture minute details invisible to human inspection. High-resolution sensors integrated into an industrial-grade camera module enable detection of microscopic defects, surface irregularities, and dimensional variations with remarkable precision. An industrial-grade camera module employs sophisticated noise reduction techniques that maintain clarity even under challenging lighting conditions or during rapid motion capture scenarios. The advanced processing capabilities embedded within an industrial-grade camera module perform real-time image analysis, instantly identifying quality anomalies and triggering corrective actions automatically. Global shutter technology featured in an industrial-grade camera module eliminates motion blur entirely, ensuring perfect image capture regardless of production line speed. The industrial-grade camera module's digital enhancement features provide operators with flexible adjustment options for contrast, brightness, and color accuracy. Integration of artificial intelligence into an industrial-grade camera module enables predictive analysis and trend monitoring that identifies potential equipment failures before they impact production quality.
Seamless Integration and Proven Reliability

Seamless Integration and Proven Reliability

An industrial-grade camera module integrates effortlessly into existing production infrastructure through standardized connectivity protocols and compatible software platforms. The industrial-grade camera module's modular design simplifies installation procedures, allowing technical teams to deploy systems rapidly without extensive facility modifications or production disruptions. Multiple interface options provided by an industrial-grade camera module ensure compatibility across diverse automation systems and legacy equipment currently operating in established facilities. An industrial-grade camera module delivers proven reliability through extensively validated designs that successfully operate across thousands of industrial installations worldwide. The industrial-grade camera module's standardized specifications facilitate straightforward procurement and simplified maintenance through readily available replacement components. Long-term support for an industrial-grade camera module includes regular firmware updates that enhance functionality while maintaining backward compatibility with existing system configurations. The industrial-grade camera module's track record demonstrates consistent performance across varied environmental conditions and demanding application scenarios encountered throughout manufacturing sectors.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000